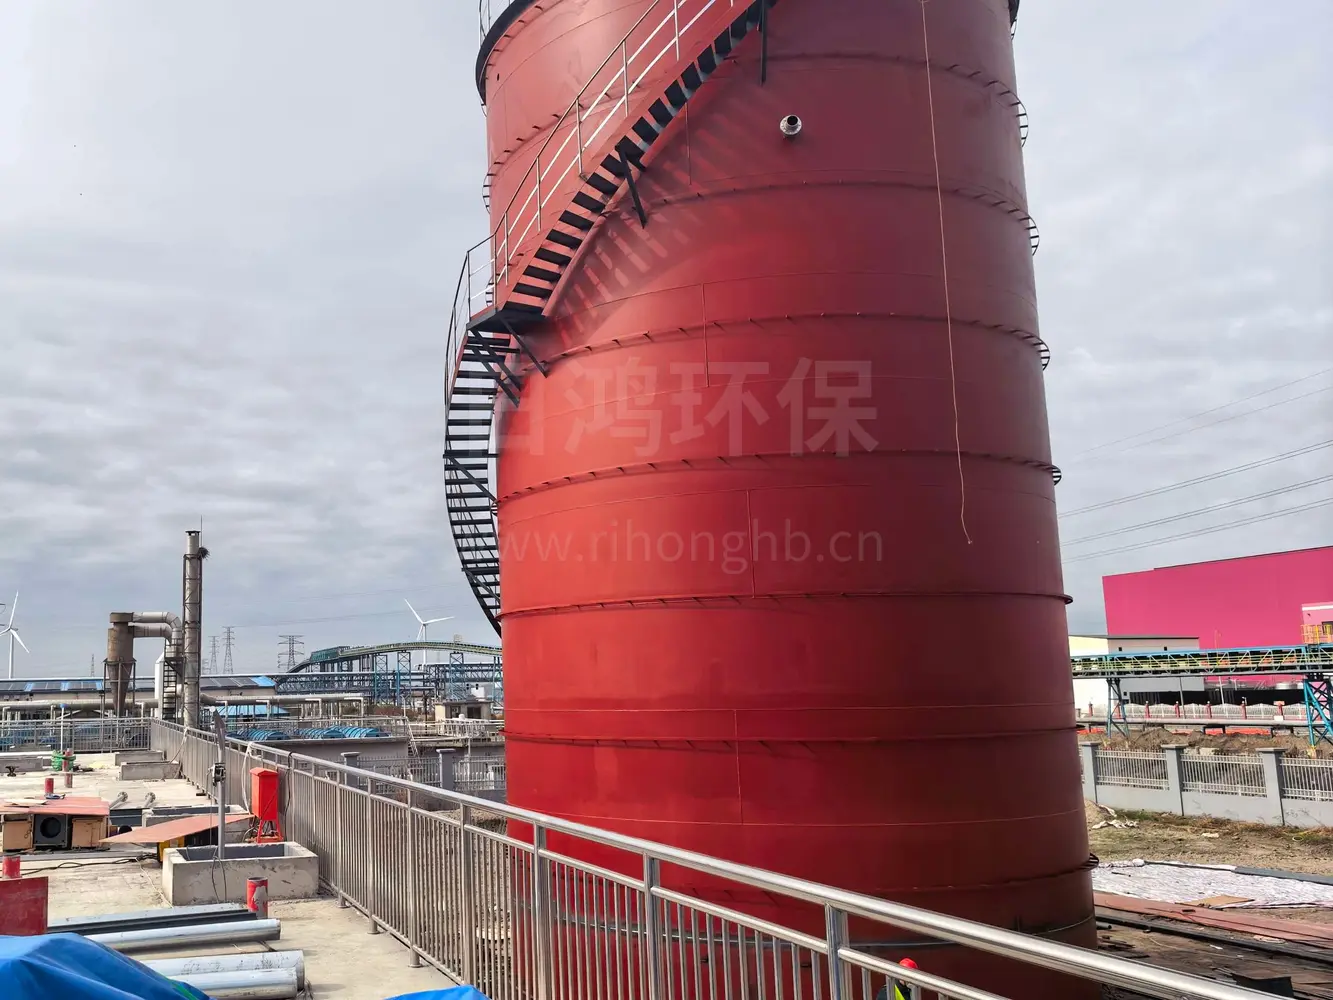
UASB Anaerobic Reactor
High-concentration organic wastewater from industries such as food, brewing, livestock farming, papermaking, and fermentation often faces the triple pressure of "high power consumption, excessive sludge, and expensive operation" when aerobic processes are used. UASB (Upflow Anaerobic Sludge Blanket) is built around a "high-concentration granular sludge bed + three-phase separator + no aeration required" and efficiently degrades organic matter within a sealed reactor while simultaneously recovering biogas. It is the preferred anaerobic unit for medium- to high-concentration organic wastewater with "pollution reduction, carbon reduction, and energy production."
I. Product Positioning
UASB is an upflow anaerobic sludge blanket reactor: wastewater flows upward from the bottom through a sludge bed composed of high-concentration anaerobic granular sludge, and organic matter is degraded step by step by anaerobic microorganisms, producing biogas; a three-phase separator is installed at the top of the reactor to efficiently separate biogas, treated water, and sludge—biogas is collected and utilized, sludge is retained and returned, and clear water overflows and is discharged. The equipment has no packing, no aeration device, and low excess sludge production, with a simple structure and stable operation. It is the mainstream high-efficiency equipment for anaerobic treatment of medium- to high-concentration organic wastewater (unlike the completely mixed CSTR, UASB relies on granular sludge and a three-phase separator to achieve high loading and short retention).
II. Working Principle (Brief)
Uniform bottom water distribution: Raw water enters uniformly from the bottom of the reactor through the distribution system and flows upward at an appropriate upflow velocity, avoiding channeling and short-circuiting.
Anaerobic degradation in the sludge bed: Wastewater flows upward through the high-concentration granular sludge bed, and organic matter is decomposed by anaerobic microorganisms, generating biogas mainly composed of methane (CH₄) and carbon dioxide (CO₂).
Three-phase separation: The mixed liquor rises to the top three-phase separator, biogas is collected and led out; sludge flocs settle by gravity, achieving efficient separation of gas, liquid, and solid phases.
Sludge retention and return: Settled granular sludge returns to the bed layer, maintaining a high biomass concentration in the reactor and ensuring stable removal under high loading.
Biogas collection and utilization: The collected biogas, after pressure stabilization and purification, can be used for power generation, boiler combustion, or flaring, achieving energy recovery and carbon emission reduction.
Clear water effluent: Clarified water overflows from the top collection trough and enters subsequent aerobic or advanced treatment units for further compliance.
Process schematic: Raw water → uniform bottom water distribution → anaerobic degradation in granular sludge bed (biogas production) → three-phase separator (gas/liquid/solid separation) → sludge return + biogas utilization + clear water effluent.
III. Core Advantages
① High loading and high efficiency The granular sludge bed has a large biomass and high volumetric loading; the COD removal rate for medium- to high-concentration organic wastewater can reach over 80%–90%.
② No aeration required, significant energy savings The anaerobic process does not consume oxygen, greatly reducing power consumption and operating costs compared with aerobic processes.
③ Biogas production and energy recovery Organic matter degradation simultaneously produces methane, which can be used for power generation or combustion, turning waste into energy and adding carbon reduction benefits.
④ Low excess sludge Anaerobic sludge production is far lower than aerobic, significantly reducing sludge disposal volume and cost.
⑤ No packing, easy maintenance Simple structure, no clogging risk; the three-phase separator integrates separation and sludge return, making management convenient.
⑥ Small footprint, strong adaptability High loading results in a small footprint; mesophilic conditions (about 35°C) provide the best efficiency, and stable operation is also possible at ambient temperature.
IV. Main Technical Parameters (Typical Range Reference)
Item | Typical Range / Description |
|---|---|
Applicable COD concentration | About 1500 mg/L and above (medium- to high-concentration organic wastewater) |
Volumetric loading (mesophilic) | About 5 – 15 kgCOD/(m³·d) (depending on water quality and temperature) |
Hydraulic retention time (HRT) | Several hours to several days (depending on concentration and design) |
Operating temperature | Mesophilic about 30–38°C (preferably 35°C±2); or ambient temperature |
COD removal rate | About 80% – 90% or above (depending on biodegradability) |
Biogas yield | About 0.35 – 0.5 m³/kgCOD(removed) |
Methane content in biogas | About 50% – 70% |
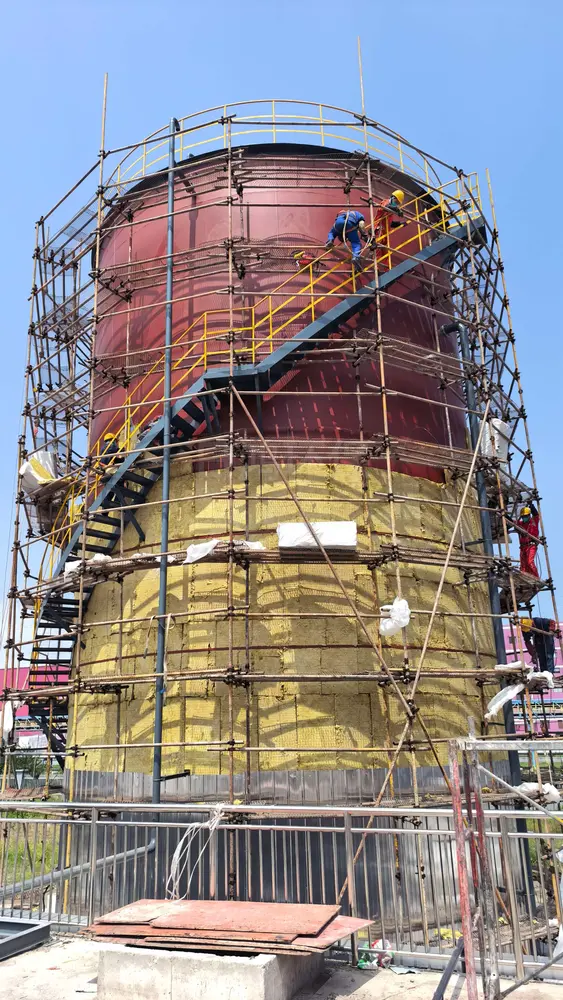
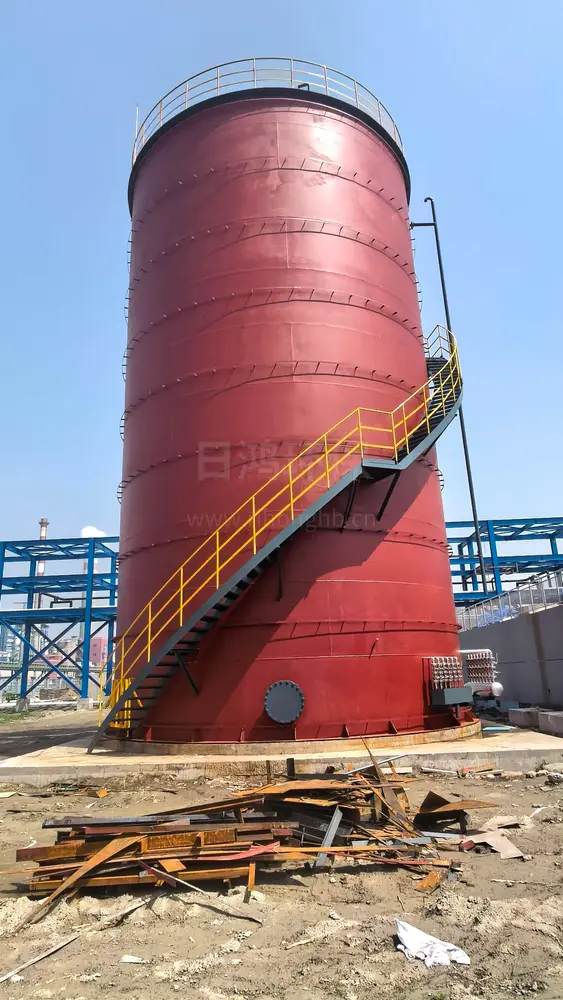
Main body form | Steel/concrete reactor, equipped with water distribution system and three-phase separator |
Layout form | Above-ground tank or underground tank, can be arranged indoors or outdoors |
Note: The above are typical engineering range reference values. Actual operation is affected by influent concentration, biodegradability, temperature, alkalinity, and inoculated sludge, and the specific values should be determined by design calculation and startup commissioning.
V. Typical Application Scenarios
Industry / Wastewater Type | Applicability Description |
|---|---|
Food / brewing wastewater | Starch, sugar refining, beer, beverages, etc., high COD, easily degradable |
Livestock / slaughterhouse wastewater | High-concentration organic, containing suspended solids, anaerobic pre-treatment for load reduction |
Paper / pulping wastewater | High-concentration organic, inhibitory substance concentrations need to be controlled |
Fermentation wastewater | Citric acid, monosodium glutamate, amino acids, etc., good biodegradability |
Some chemical / pharmaceutical organic wastewater | For those with good biodegradability, inhibitors need to be prevented |
Landfill leachate | Anaerobic pre-treatment, reducing load and improving biodegradability |
Municipal sludge digestion liquor | Connected with anaerobic digestion and biogas slurry treatment |
VI. Applicable Boundaries and Selection Recommendations
Suitable for: Medium- to high-concentration organic wastewater with good biodegradability; projects that seek "pollution reduction + biogas energy recovery" and are sensitive to footprint and power consumption. The statement "low-concentration wastewater is not economical, and completely mixed processes such as CSTR should be selected" is the reverse: UASB is more suited to medium- to high-concentration, high-loading, short-retention scenarios.
Points to note: ① It is relatively sensitive to suspended solids (SS), sulfate, ammonia nitrogen, and toxic inhibitors, so influent water quality regulation and pretreatment are required; ② Low temperature significantly reduces efficiency, so insulation or heating to mesophilic operation is recommended; ③ Anaerobic effluent still contains pollutants and must be connected to aerobic/advanced treatment to meet standards; ④ The startup period requires a relatively long process of sludge inoculation, acclimation, and granulation, so a commissioning period should be reserved; ⑤ It should be distinguished from CSTR—UASB has no mixing, relies on granular sludge and a three-phase separator, has high loading and short retention, and is less tolerant of solids-containing/viscous materials than CSTR.
Selection recommendations: Determine loading and volume according to influent COD, biodegradability, and temperature; give priority to mesophilic operation; emphasize uniform water distribution and three-phase separator design; and plan comprehensively with subsequent aerobic treatment and biogas purification/utilization.
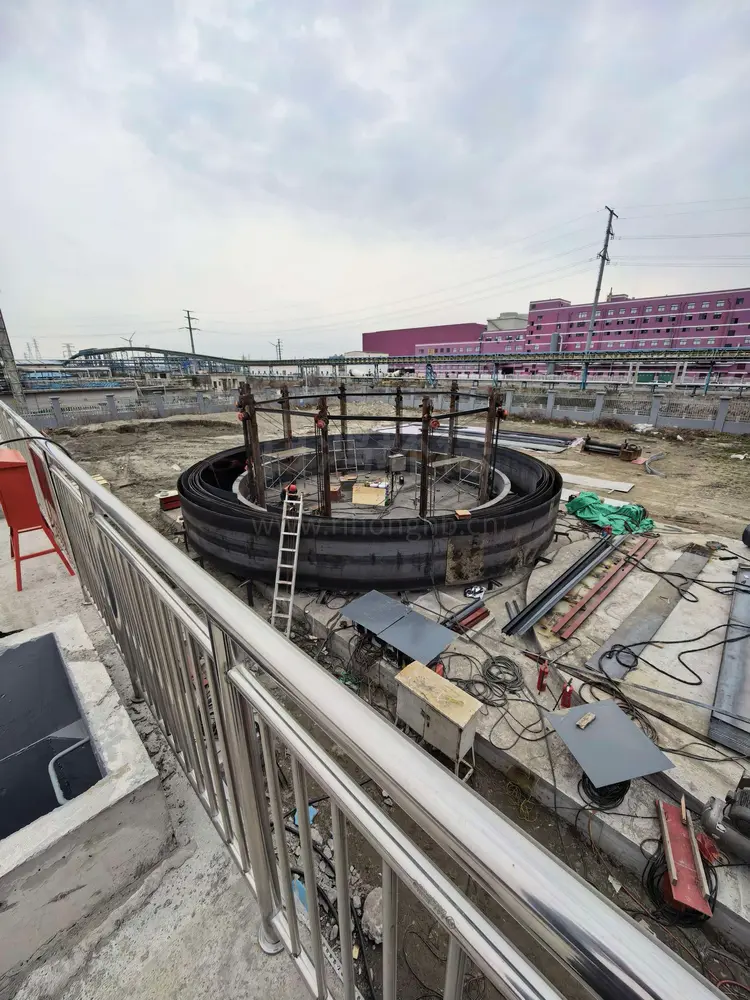
Product Images
FAQ
How much does this equipment cost?
The price varies by treatment capacity, water quality, materials and configuration, so a custom quote is provided based on your actual conditions. We offer free water testing and solution design, with a detailed quote within 1 working day after requirements are confirmed.
What treatment capacity is available? Can it be customized?
Capacity is fully customizable, ranging from tens to thousands of tons per day (e.g. 0.5–30 m³/h), with non-standard design support matched precisely to your inlet/outlet requirements.
How long does delivery take?
Standard equipment typically takes about 2–4 weeks to produce; custom projects depend on scale and process. The delivery date is confirmed at contract signing, with design, manufacturing and shipping progressing on schedule.
Is installation and commissioning included?
Yes. We provide installation, system commissioning, operator training and environmental acceptance assistance, as well as long-term managed operation services on request.
What about after-sales and warranty?
We provide a warranty period and a 24/7 technical hotline, with free repair for non-human faults during the warranty period, plus spare parts supply and regular inspection services.
Still worried about wastewater treatment?
We can provide volumetric loading calculations, water distribution and three-phase separator design, and startup commissioning plans. Provide water quality and quantity, and we will give configuration recommendations for your project.
Contact Us Now →Related Products
CSTR Anaerobic Reactor
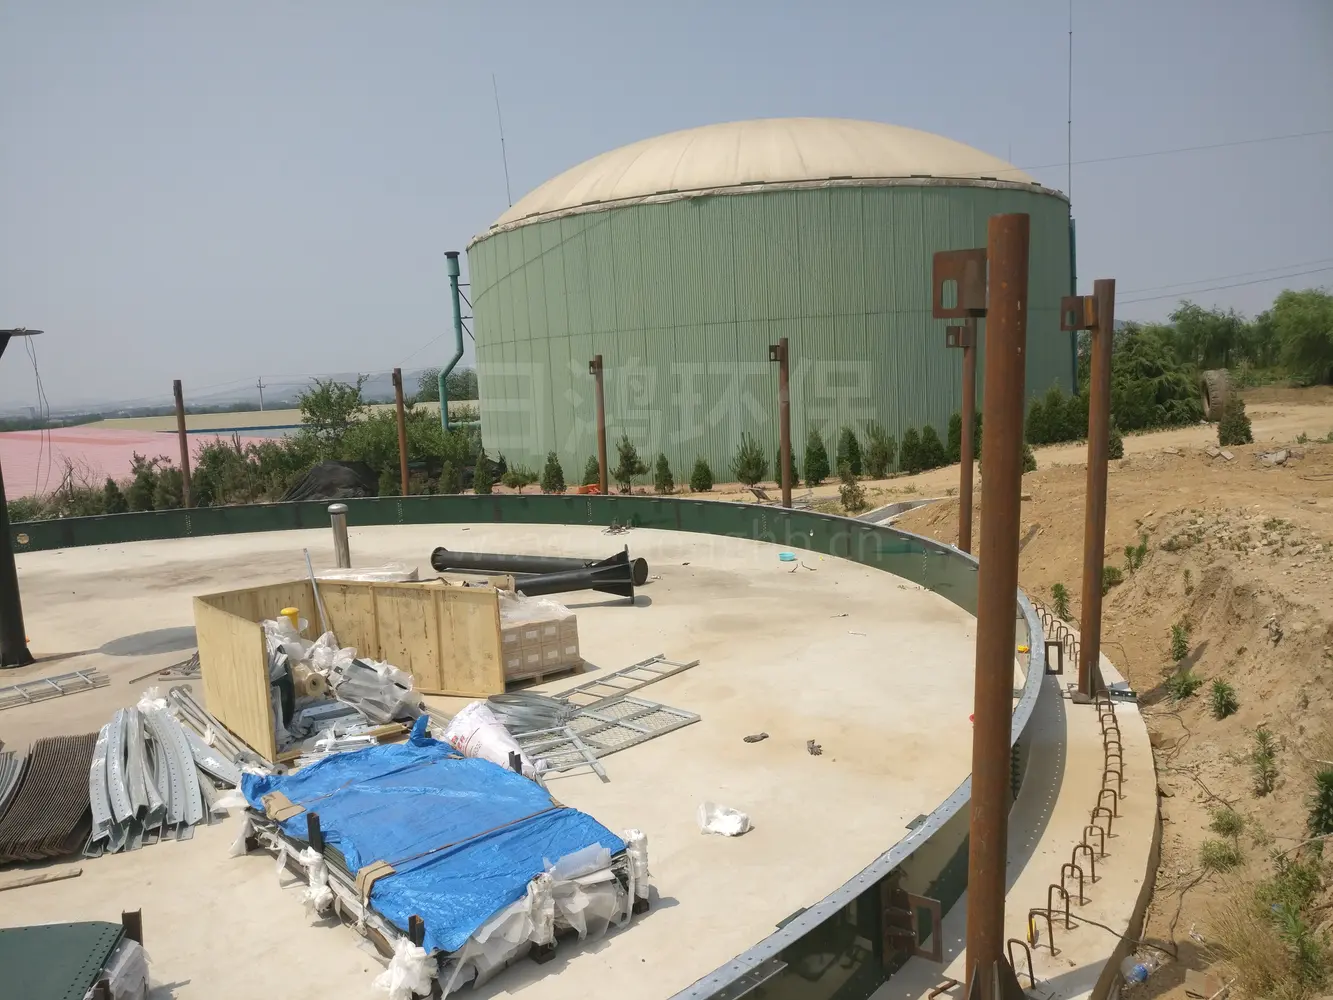
For high-concentration organic wastewater from alcohol, starch, slaughterhouse, livestock, and food processing that is difficult for biochemical pretreatment, as well as the reduction and disposal of municipal sludge and food waste, traditional aerobic processes have high energy consumption and large sludge production. CSTR (Continuous Stirred Tank Reactor) is centered on "fully mixed stirring + mesophilic/thermophilic anaerobic digestion + biogas energy recovery," converting organic matter into clean energy biogas within a sealed tank, achieving the dual benefits of "pollution reduction" and "energy production."
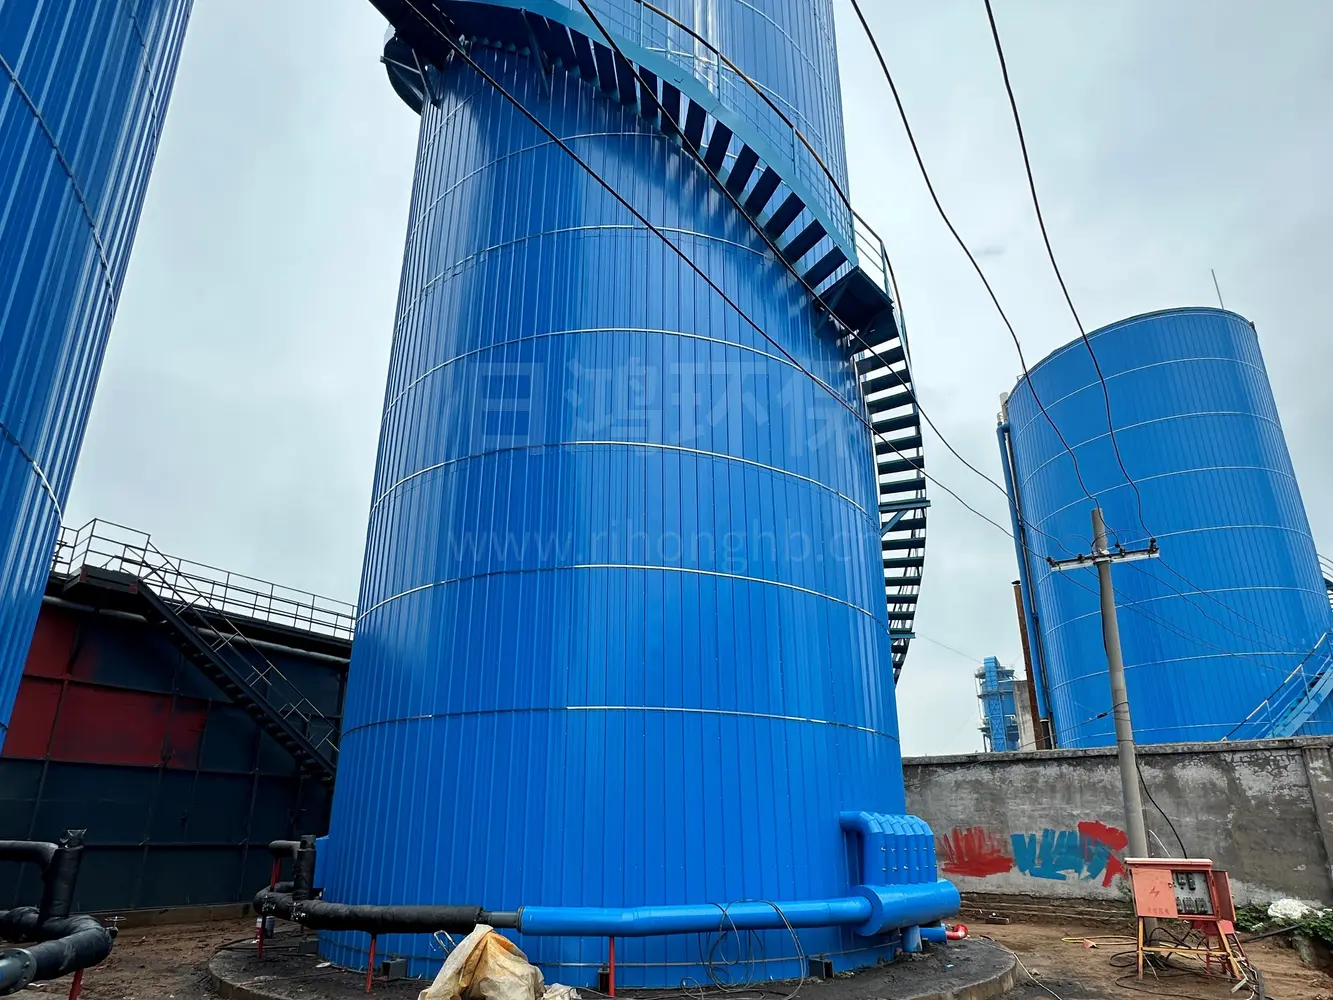
IC Anaerobic Reactor Tower
When treating medium- to high-strength organic wastewater, the goals of "high loading, small footprint" must be balanced with stable operation and energy recovery—yet conventional UASB is already approaching its loading limit. The IC (Internal Circulation) anaerobic reactor is built around a "high height-to-diameter ratio tank + two-stage reaction chambers + biogas-driven internal circulation." Using biogas production as the driving force, it forms a sludge-water circulation inside the reactor, greatly improving mass transfer efficiency and volumetric loading. It is the preferred high-efficiency anaerobic equipment for industries such as brewing, starch, papermaking, and chemicals.