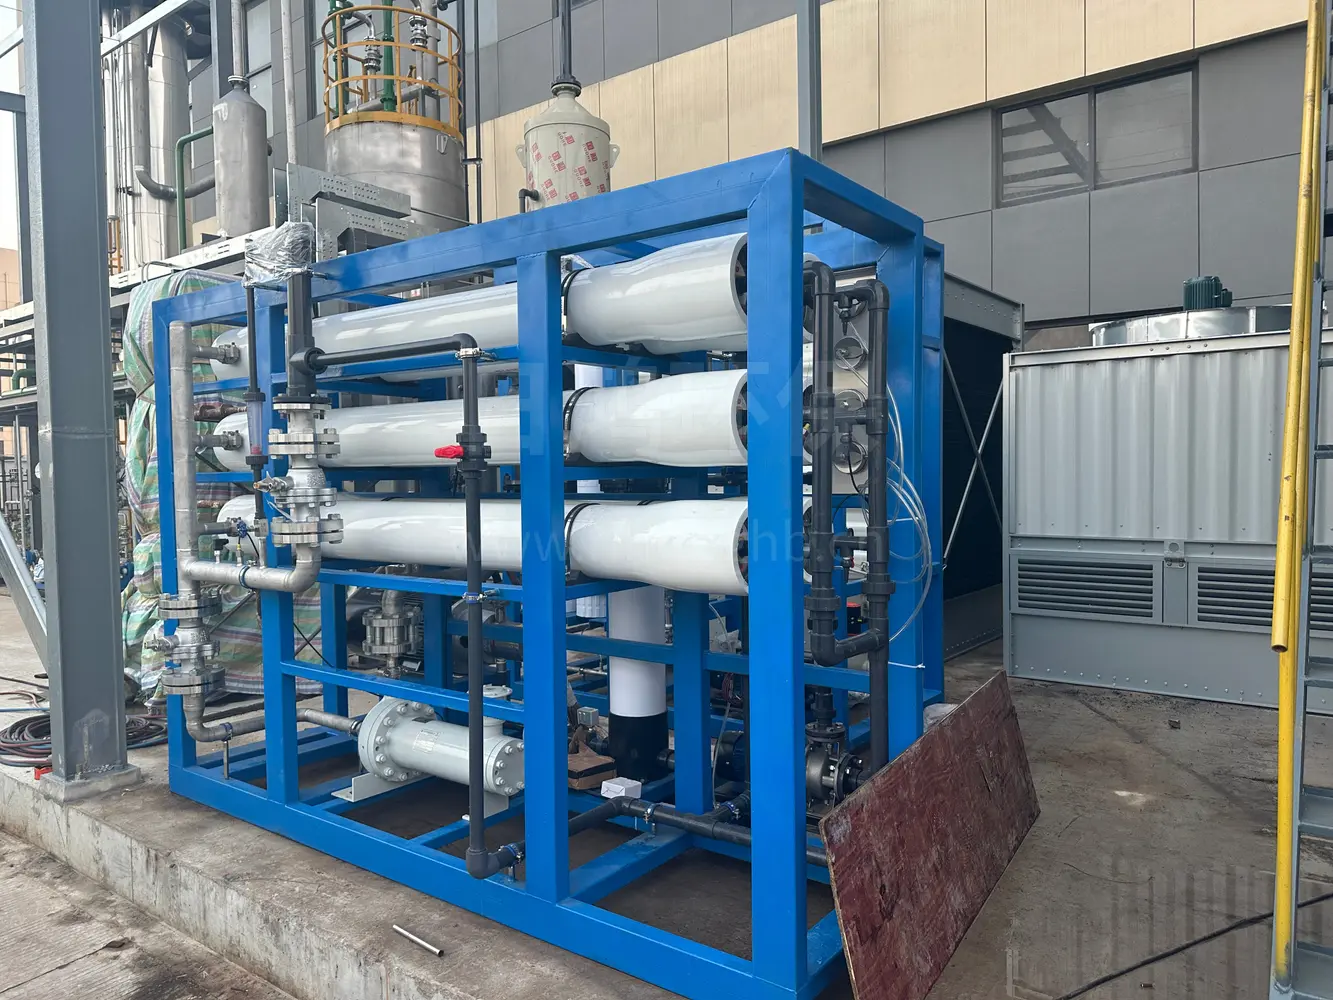
Reclaimed Water Reuse RO Reverse Osmosis System
As industrial water intake costs rise and discharge standards tighten, "less fresh water intake, less wastewater discharge" has become a rigid demand. Direct discharge of municipal reclaimed water or a company's own secondary treated effluent is both wasteful and consumes quota. Wushi Environmental launches the industrial reclaimed water reuse RO reverse osmosis system, with Ultrafiltration (UF) + Reverse Osmosis (RO) dual-membrane process as the core, stably converting reclaimed water into circulating cooling make-up water, process water, and even boiler feedwater, with recovery up to 70% – 85%. The concentrate can enter evaporation crystallization to approach zero liquid discharge, helping enterprises save water, reduce emissions, and lower costs.
I. Product Positioning
The reclaimed water reuse RO system is core equipment for wastewater resource recovery via membrane technology, targeting "near-compliant" water sources such as municipal reclaimed water and industrial wastewater secondary treated effluent. It adopts a UF pre-treatment + anti-fouling RO membrane dual-membrane process: UF retains suspended solids, colloids, and microorganisms, while RO retains dissolved salts, hardness, organic matter, and microorganisms, with product water reused and concentrate reduced. The system integrates pre-treatment, high-pressure pump, anti-fouling membrane stack, energy recovery (optional), and automatic control system. It is a reliable choice for industrial circulating water make-up, process reuse, and front-end pre-concentration for zero liquid discharge (ZLD).
II. Working Principle (Brief)
Reclaimed water intake / conditioning: Receives municipal reclaimed water or enterprise secondary treated effluent, homogenizes flow and quality, stabilizes influent load.
Dual-membrane pre-treatment: UF ultrafiltration removes suspended solids, colloids, and microorganisms, with softening / scale inhibition / pH adjustment to protect RO membranes and delay fouling (multi-media + carbon filtration + cartridge filtration can also be used).
High-pressure pump pressurization: Provides operating pressure for RO (approximately 1.5 – 4.0 MPa depending on influent salinity), driving water molecules through the semi-permeable membrane.
RO membrane separation: Anti-fouling spiral-wound membranes retain salts, hardness, organic matter, and microorganisms under high pressure, separating product water and concentrate.
Product water reuse: Product water is used as circulating cooling make-up water and process water; for higher requirements such as boiler feedwater, it can be further purified by EDI / mixed bed.
Concentrate disposal: High-salinity concentrate goes to evaporation crystallization / electrodialysis (ED) or compliant discharge, achieving reduction and approaching zero liquid discharge.
Process schematic: Reclaimed water → UF pre-treatment (softening/scale inhibition) → High-pressure pump → RO membrane separation → Product water reuse (→ EDI/mixed bed); Concentrate → Evaporation/ED/discharge
The dual-membrane process is primarily physical separation with no large chemical dosage: UF guards the RO influent SDI red line, and anti-fouling RO stably produces water at high recovery rates. It saves water and reduces pollution load, making it a mature path for industrial wastewater resource recovery.
III. Core Advantages
① Stable dual-membrane process, shock-resistant UF pre-treatment + anti-fouling RO, resistant to reclaimed water quality fluctuations, stable operation.
② High recovery, significant water savings Recovery rate 70% – 85%, greatly reducing fresh water intake and wastewater discharge.
③ High desalination, controllable water quality Product water meets circulating cooling / process / boiler feedwater requirements, desalination rate ≥ 99%.
④ Pollution and emission reduction, approaching zero discharge Concentrate can enter evaporation crystallization, supporting enterprises' zero liquid discharge (ZLD) goals.
⑤ Skid-mounted integration, plug-and-play Pre-treatment + pump + membrane + control integrated, produces water upon connecting water and power on site.
⑥ Intelligent control, unattended operation Automatic flushing / CIP, high-low pressure protection, and online water quality monitoring, simple operation and maintenance.
IV. Main Technical Parameters (Range Reference)
Item | Parameter Range / Description | Remarks |
|---|---|---|
Product water capacity | Approx. 5 – 500 m³/h (multiple units can be paralleled for expansion) | According to reuse demand |
Influent water quality | Municipal reclaimed water / industrial wastewater secondary treated effluent (must meet pre-treatment red line) | Control COD/SS/hardness/residual chlorine/SDI |
Desalination rate | ≥ 99% (for dissolved salts) | Single-stage RO |
Operating pressure | Approx. 1.5 – 4.0 MPa | Varies with influent TDS, seawater membrane for high salinity |
System recovery rate | Approx. 70% – 85% | Concentrate reduction |
Product water quality | Meets GB/T 19923 industrial circulating cooling water make-up or enterprise internal control standards | Can be further purified by EDI |
Membrane element | Anti-fouling spiral-wound brackish water RO membrane (BWRO); seawater membrane for high salinity | Dual-membrane UF + RO |
Pre-treatment | UF ultrafiltration + softening / scale inhibition + cartridge filtration | Key to membrane protection |
Power consumption per ton of water | Approx. 1.0 – 3.0 kWh/m³ | Varies with pressure and recovery rate |
Main material | Anti-corrosion carbon steel / stainless steel, membrane housing FRP / stainless steel | According to medium |
* The above are typical range reference values. Actual recovery rate, product water quality, and energy consumption vary with influent water quality, membrane model, and operating conditions; influent must meet pre-treatment standards. Specific values are determined by design calculation and water quality testing.
V. Typical Application Scenarios
Industry / Process | Main Use |
|---|---|
Power / Steel | Circulating cooling system make-up water, replacing large amounts of fresh water |
Electronics / Electroplating | High-purity water for cleaning and rinsing (with EDI / mixed bed) |
Printing and Dyeing / Textile | Advanced treatment and reuse of printing and dyeing wastewater |
Chemical / Petrochemical | Process and water system reuse, water saving and emission reduction |
Paper Making | White water / mid-stage water reuse |
Park / Development Zone | Centralized reclaimed water treatment and unified reuse |
Zero Liquid Discharge (ZLD) front-end | Pre-concentration and reduction, lowering evaporation load |
VI. Selection Recommendations
Reclaimed water reuse RO is suitable for advanced reuse and resource recovery of "near-compliant" water sources such as municipal reclaimed water or industrial secondary effluent; its influent must meet biological / physicochemical pre-treatment standards (COD, SS, hardness, residual chlorine, SDI not exceeding limits), otherwise membranes are prone to fouling or oxidation. The concentrate has high salinity and must have a compliant destination (evaporation crystallization, electrodialysis, or compliant discharge), and should not be directly discharged; high TDS water sources require high-pressure / seawater membranes, with correspondingly higher energy consumption. Selection should be calculated based on influent water quality, reuse standards, and recovery rate targets, and space should be reserved for membrane cleaning, energy recovery, and spare parts to ensure long-term stable and economical operation.
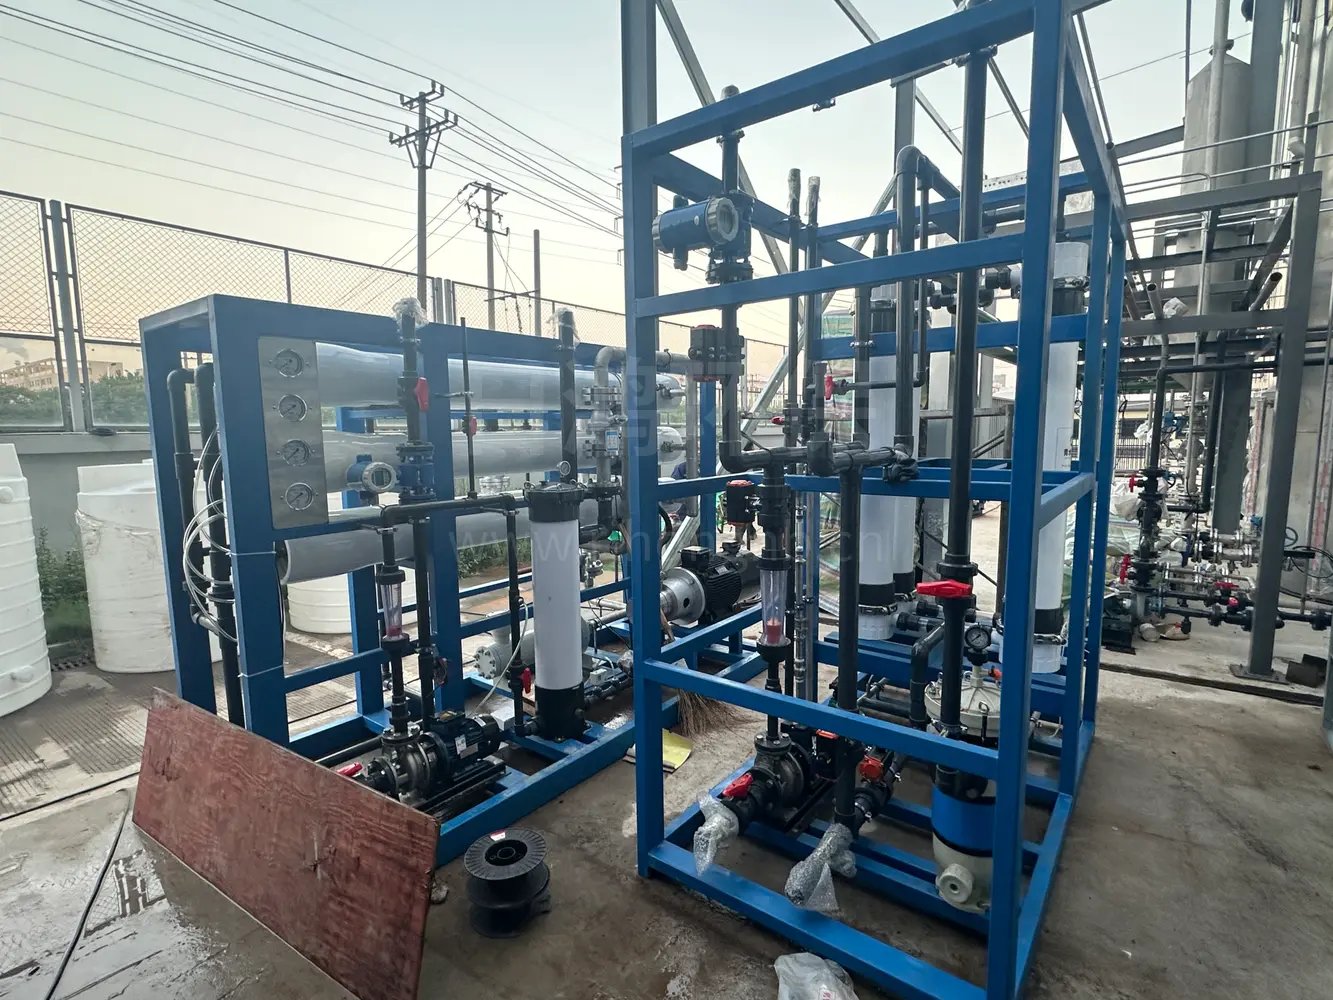
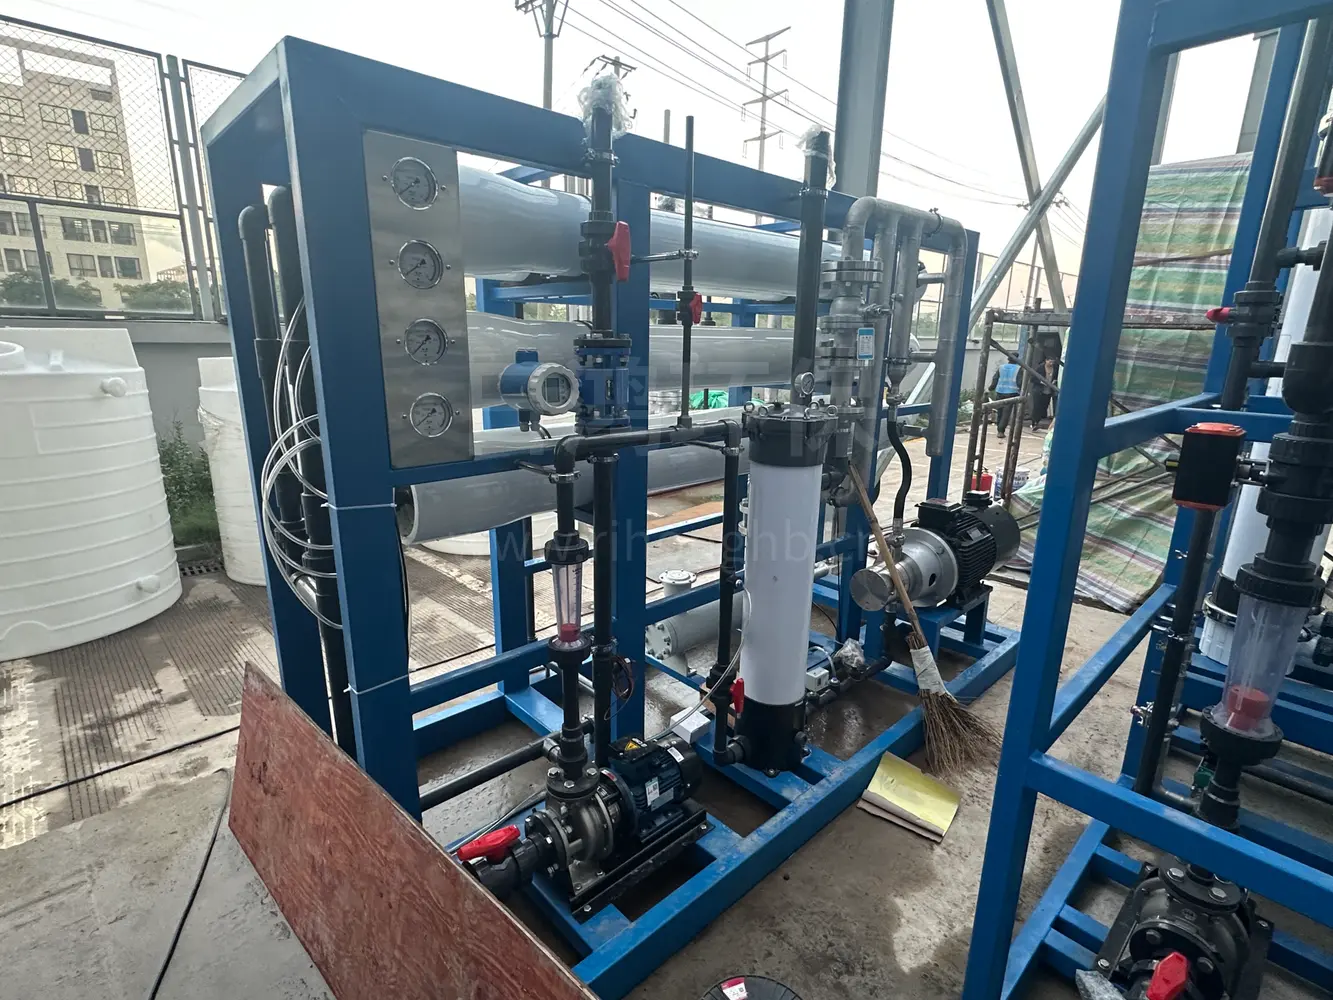
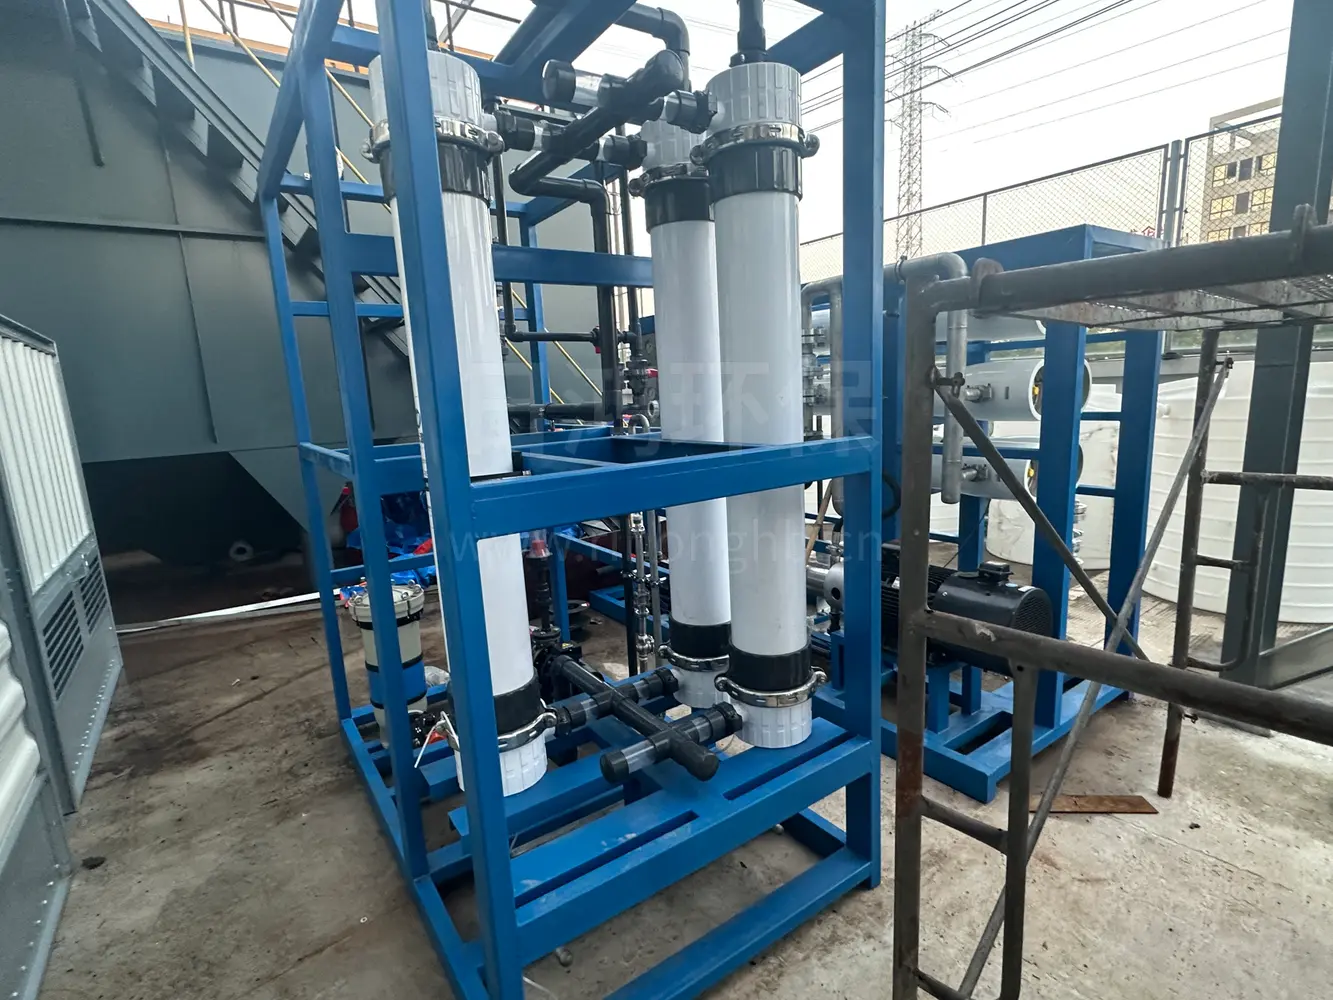
Product Images
FAQ
How much does this equipment cost?
The price varies by treatment capacity, water quality, materials and configuration, so a custom quote is provided based on your actual conditions. We offer free water testing and solution design, with a detailed quote within 1 working day after requirements are confirmed.
What treatment capacity is available? Can it be customized?
Capacity is fully customizable, ranging from tens to thousands of tons per day (e.g. 0.5–30 m³/h), with non-standard design support matched precisely to your inlet/outlet requirements.
How long does delivery take?
Standard equipment typically takes about 2–4 weeks to produce; custom projects depend on scale and process. The delivery date is confirmed at contract signing, with design, manufacturing and shipping progressing on schedule.
Is installation and commissioning included?
Yes. We provide installation, system commissioning, operator training and environmental acceptance assistance, as well as long-term managed operation services on request.
What about after-sales and warranty?
We provide a warranty period and a 24/7 technical hotline, with free repair for non-human faults during the warranty period, plus spare parts supply and regular inspection services.
Still worried about wastewater treatment?
Free Testing · Free Custom Solutions · Engineering Construction · Equipment R&D · Managed Operation
Contact Us Now →Related Products
Integrated Water Purifier
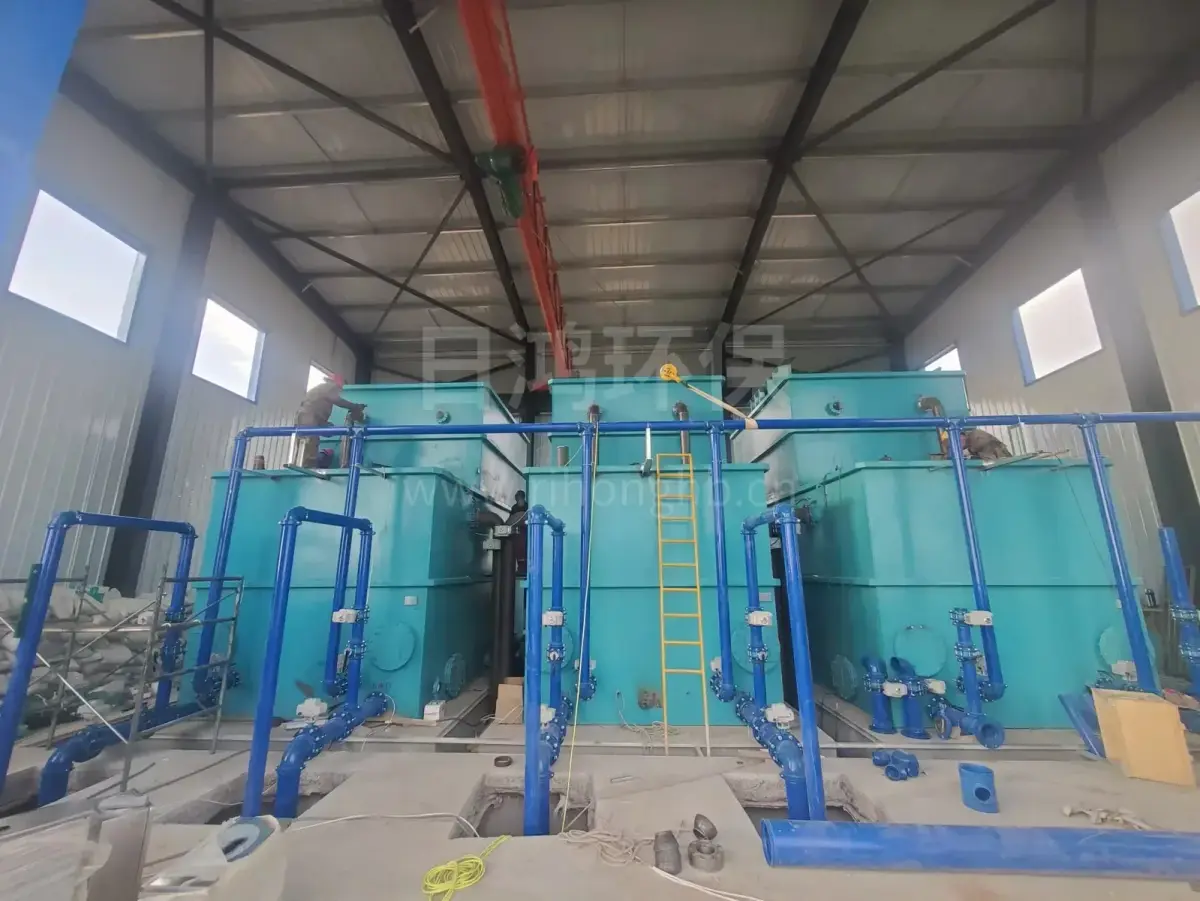
In rural areas, towns, military camps, factories and mines, surface water sources are scattered, and building traditional water treatment plants often faces challenges such as large investment, extensive land occupation, and long construction periods. Wushi Environmental Protection introduces the Integrated Water Purifier, which integrates coagulation, flocculation, sedimentation, filtration, and disinfection of a conventional water plant into a single ground-mounted unit. The effluent consistently meets the Standards for Drinking Water Quality (GB 5749), enabling scattered point sources to access safe and stable tap water.
RO Reverse Osmosis System for the Food Industry
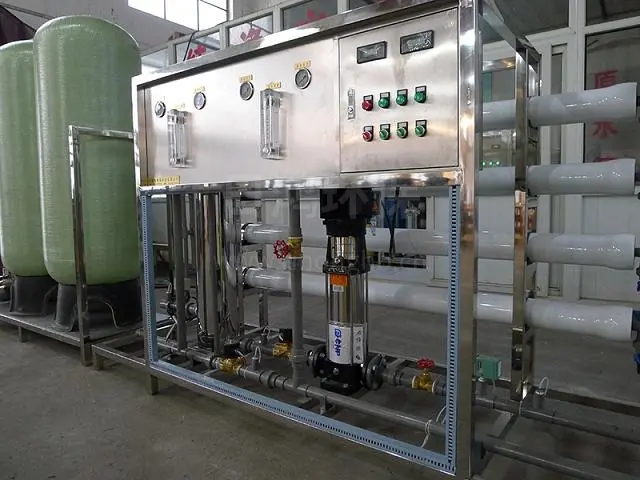
Beverage, brewing, dairy, canning and other food production processes have extremely high requirements for the quality, stability and food safety of process water, while municipal water or groundwater often contains salinity, hardness, residual chlorine and microorganisms. Wushi Environmental has launched RO reverse osmosis equipment for the food industry, integrating pretreatment, high-pressure pumps, membrane separation and automatic control into a single skid-mounted unit. It performs physical desalination at ambient temperature without the need for large amounts of chemicals, stably producing high-purity process water to help food enterprises meet water quality standards, improve quality and reduce costs.
Valveless Filter
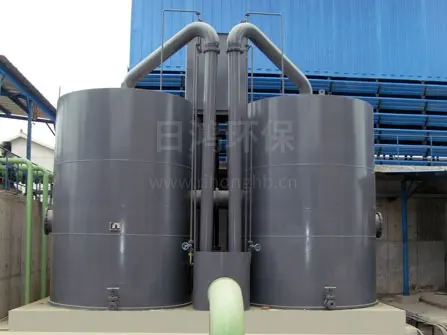
Traditional rapid filters have many valves, complex operation, and rely on manual timing for backwashing, resulting in heavy O&M burden and prone to misoperation. The valveless filter uses the "siphon principle" to replace all valves, achieving a fully automatic filtration-backwash cycle without the need for dedicated personnel. It is an economical choice for rural water supply, industrial circulating water side-stream filtration, and advanced filtration for reclaimed water reuse.
Microsand and Carbon Sedimentation Tank
Faced with the challenge of "dissolved taste and odor, color, micropollutants, and refractory COD" in drinking water and reuse water that cannot be removed by conventional coagulation and sedimentation, and with limited plant footprint, the Microsand and Carbon Sedimentation Tank couples microsand-loaded high-rate sedimentation with powdered activated carbon (PAC) adsorption in a single unit. It efficiently removes turbidity while adsorbing dissolved pollutants, with microsand recycled for reuse, requiring only 1/5–1/10 of the footprint of traditional processes.